Punching is back
Produza mais. Reduza os tempos de preparação.
É possível carregar 38 ferramentas em simultâneo, permitindo executar famílias completas de trabalhos de armários sem interrupções. Sem troca manual de ferramentas durante o processo. Menos mudanças de preparação. Mais peças por turno.
±0,1 mm. Turno após turno
A estrutura de processamento SHW e o servossistema de circuito fechado garantem uma precisão de puncionamento de ±0,1 mm durante o puncionamento contínuo de alta frequência, sem desvios ao longo do tempo. Precisão que pode garantir aos seus clientes.
Menos desperdício. Tempos de ciclo mais curtos.
O nesting, o cálculo de custos e o sequenciamento integrados proporcionam uma utilização do material 8–15% superior à disposição manual. Sem cortes de teste nem desperdício de chapa. Tempos de ciclo automaticamente mais curtos.
Programação em piloto automático
O JFY PUNCH programa automaticamente as peças a puncionar, com otimização da sequência, ferramentas agrupadas, microjuntas e sem introdução manual de dados. Ligue-se ao JFY PLUS e programe corte, puncionamento e quinagem numa única interface e num único fluxo de trabalho.
Formas que nenhum laser consegue produzir
Grelhas, repuxos, furos roscados, nervuras e recortes: tudo num único programa e numa única máquina. Se as suas peças necessitam de conformação, só o puncionamento a consegue realizar.
Caraterísticas e desempenho
Detalhes
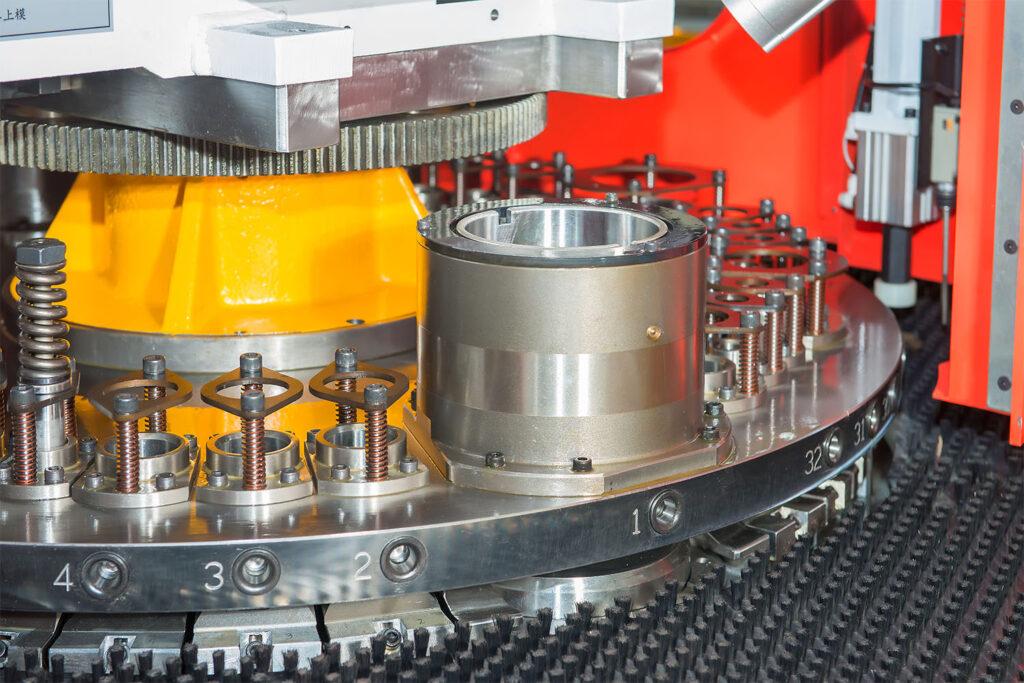
38-station turret
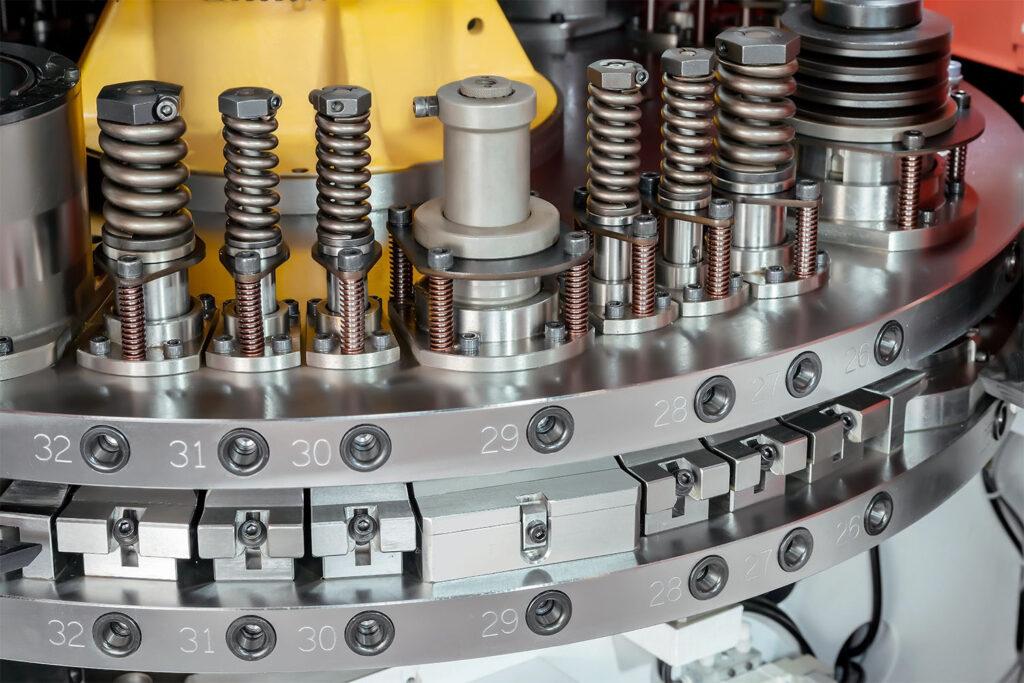
Keep punching, forming, louver and tools loaded at the same time. Fewer tool changes keep batch jobs running instead of waiting for setup.
38 stations for a broad mix of punching and forming tools.
Quick-release lower dies simplify between-job changes.
Supports longer runs with fewer manual interruptions
Auto-index rotary station
Produce angled louvers, lances and other directional forms under CNC control. The tool rotates through 360 degrees, avoiding separate tools for every orientation.
Less duplicate tooling and lower risk of loading the wrong tool.
Rotary operations remain part of the CNC program.
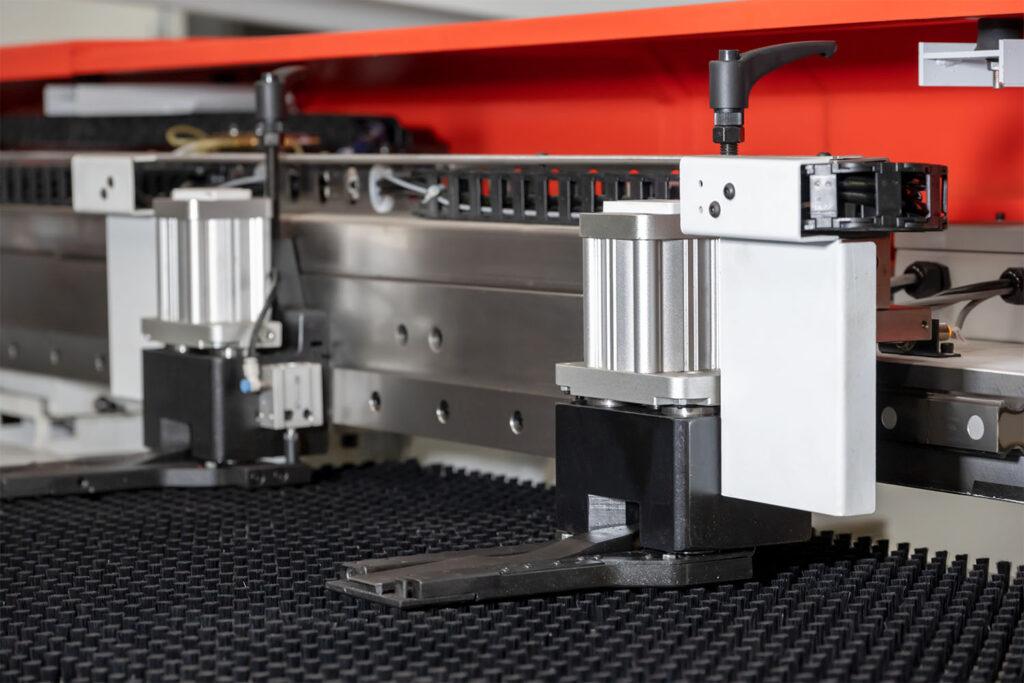
Floating clamp system
Keep the sheet controlled while allowing the required movement during processing. Material-drop detection and clamp protection stop the machine before a misaligned sheet or unsafe stroke causes damage.
Detects sheet movement before the next punch stroke.
Position monitoring helps prevent die-to-clamp collisions.
Protects long nested runs with less operator supervision.
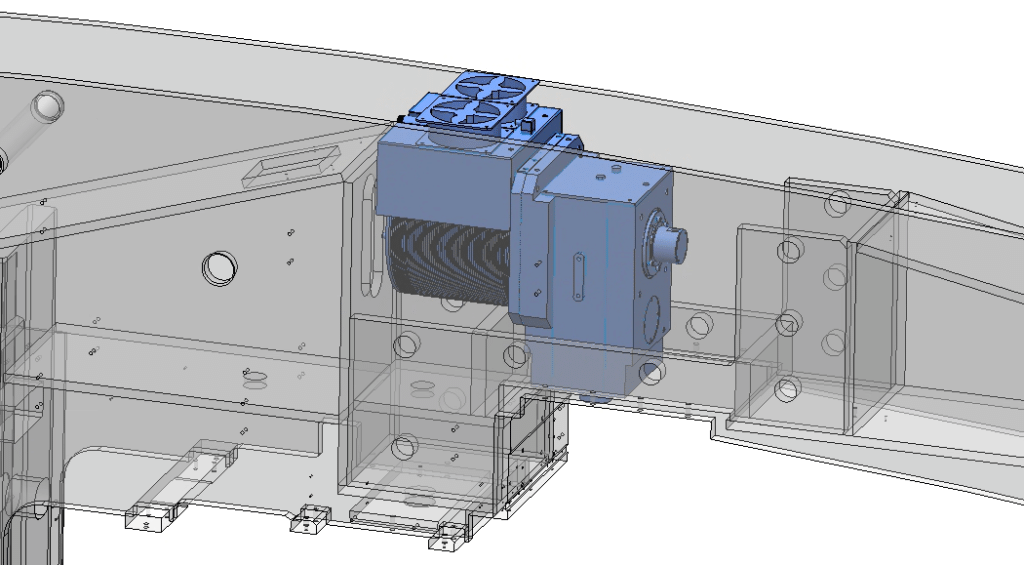
Servo punching drive
The direct-drive servo delivers punching power immediately and uses energy in proportion to the work performed. Air cooling and closed-loop control support stable, repeatable forming.
High-torque direct-drive motor with overload capacity.
Air cooling avoids coolant-related service concerns.
Closed-loop control keeps the forming depth consistent.
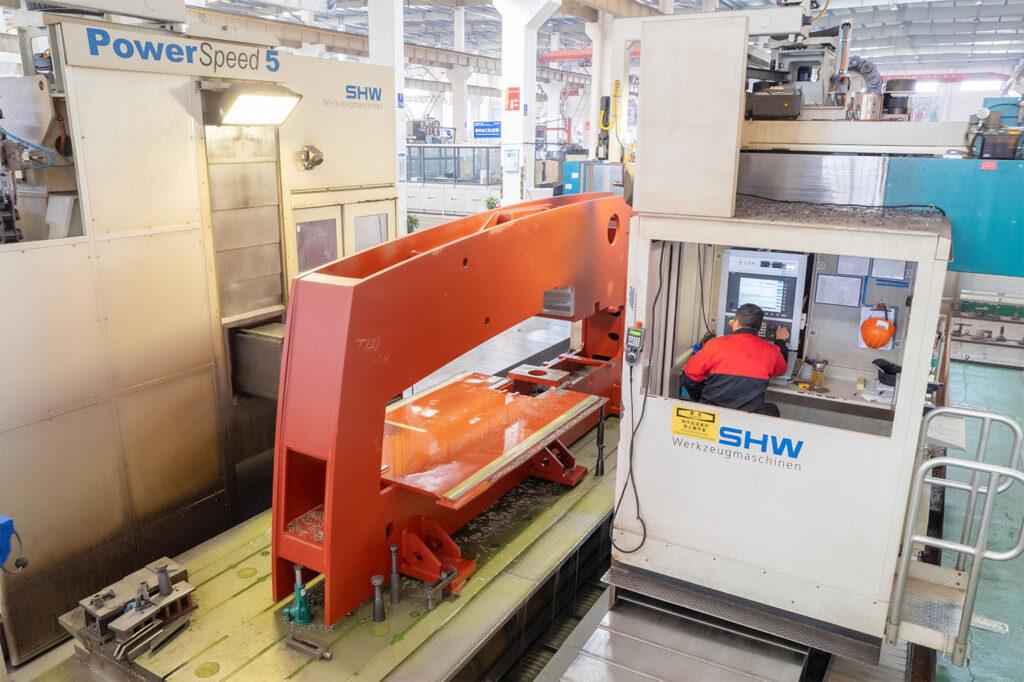
Machine frame
The closed welded frame, five-face SHW machining and finite-element design help keep the machine geometry stable during high-frequency punching. A common coordinate system supports consistent accuracy across the shift.
Rigid closed structure designed to resist deformation.
Key reference surfaces are machined in one coordinate system.
Supports the specified ±0.1 mm punching accuracy.
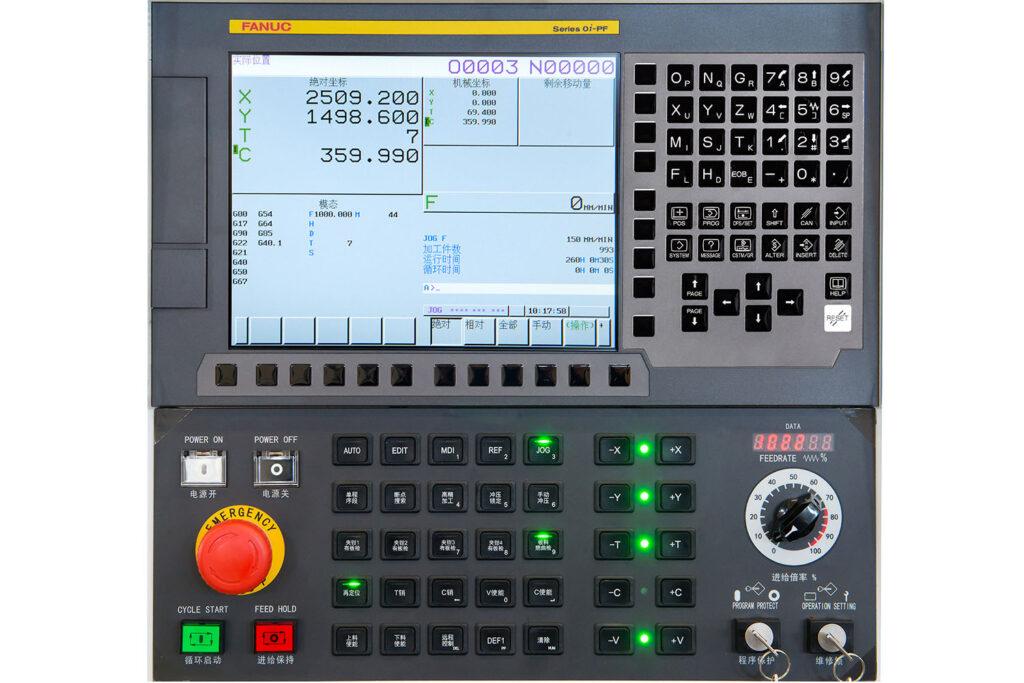
FANUC CNC system
A familiar CNC platform simplifies operation, maintenance and support. Existing FANUC experience can transfer to the MT300E without learning a proprietary control environment from scratch.
Five controlled axes: X, Y, V, T and C.
Familiar diagnostics and service practices.
FANUC support infrastructure is available across major markets.
Dados técnicos
| Specification | MT+ 300E-2515 |
|---|---|
| Max. punch force | 300 kN |
| Tipo de acionamento principal | Servo motor |
| Dimensão máxima de processamento de folha (com reposicionamento único) | 5000x1500 mm |
| Espessura máxima de processamento da chapa | 6 mm |
| Max. punch diameter per time | Φ88.9 mm |
| Curso máx. de puncionamento | 32 mm |
| No. of clamps | 3 unidades |
| No. of stations | 32 pcs |
| Número de índices automáticos | 2 (C) pcs |
| Precisão de puncionamento | ±0.1 mm |
| Max. feeding speed - X Axis | 80 m/min |
| Max. feeding speed - Y Axis | 80 m/min |
| Max. feeding speed - XY Combined | 113 m/min |
| Worktable Selection - For thickness 3 mm and below | Fine brush fixed worktable |
| Worktable Selection - For thickness 3-4 mm | Brush and steel ball fixed worktable |
| Worktable Selection - For thickness 4-6 mm | All steel ball fixed worktable |
| Max. punch hit at 1 mm pitch with 6 mm stroke | 750 hpm |
| Max. punch hit at 25 mm pitch with 6 mm stroke | 400 rpm |
| Velocidade do carrossel | 30 rpm |
| Sistema CNC | FANUC |
| No. of controlling axis | 5 (X, Y, V, T, C) pcs |
| Dimension (Including safety fence) | 7026×7900×2360 mm |