Punching is back
Produceți mai mult. Reduceți timpul de configurare.
Pot fi încărcate simultan 38 de scule, astfel încât familii întregi de lucrări pentru dulapuri să poată fi executate fără întreruperi. Fără schimbarea manuală a sculelor în timpul procesului. Mai puține reconfigurări. Mai multe piese pe schimb.
±0,1 mm. Schimb după schimb
Cadrul de prelucrare SHW și servosistemul cu buclă închisă asigură o precizie de ștanțare de ±0,1 mm în timpul ștanțării continue de înaltă frecvență, fără abateri în timp. Precizie pe care o puteți garanta clienților dumneavoastră.
Mai puține rebuturi. Timpi de ciclu mai scurți.
Optimizarea integrată a dispunerii, calcularea costurilor și secvențierea asigură o utilizare a materialului cu 8–15% mai bună decât dispunerea manuală. Fără tăieri de probă și fără tablă irosită. Timpi de ciclu automat mai scurți.
Programare pe pilot automat
JFY PUNCH programează automat piesele pentru ștanțare, cu optimizarea secvenței, gruparea sculelor, micro-punti și fără introducere manuală. Conectați-vă la JFY PLUS și programați debitarea, ștanțarea și îndoirea într-o singură interfață și într-un singur flux de lucru.
Forme pe care laserul nu le poate produce
Jaluzele, nervuri, filete, rigidizări și ambutisări: toate într-un singur program și pe un singur utilaj. Atunci când piesele necesită deformare, numai perforarea oferă rezultatul dorit.
Caracteristici și performanțe
Detalii
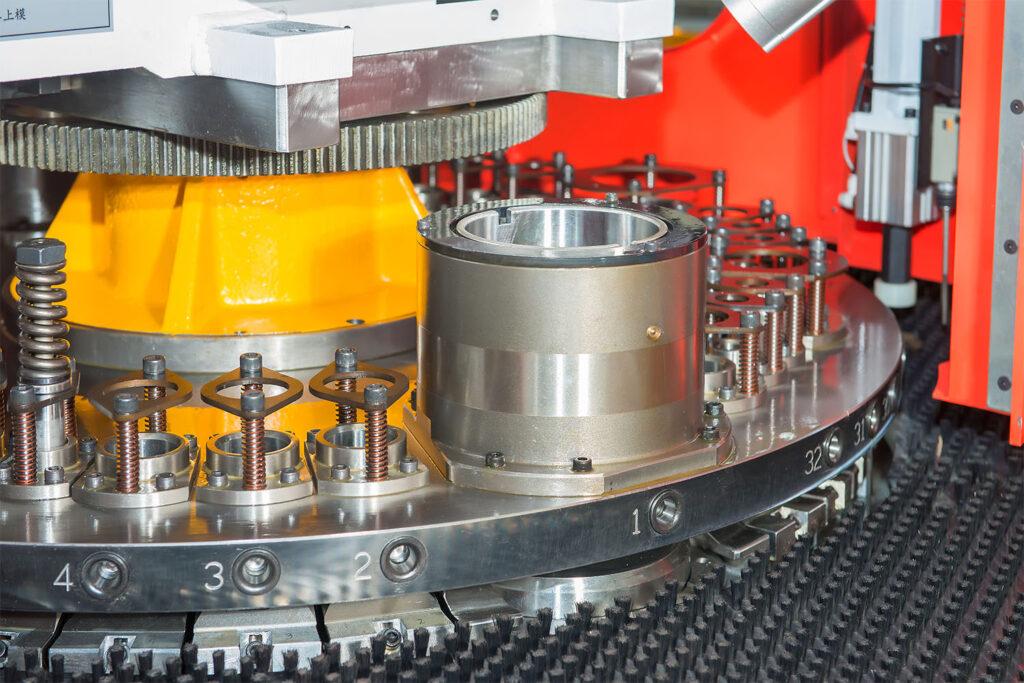
38-station turret
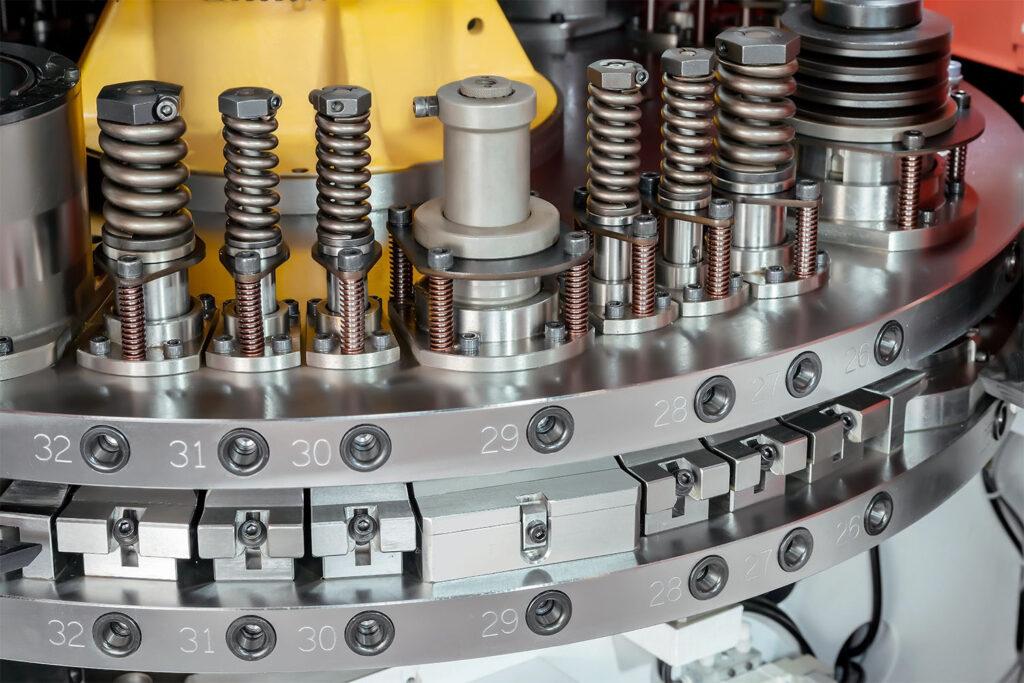
Keep punching, forming, louver and tools loaded at the same time. Fewer tool changes keep batch jobs running instead of waiting for setup.
38 stations for a broad mix of punching and forming tools.
Quick-release lower dies simplify between-job changes.
Supports longer runs with fewer manual interruptions
Auto-index rotary station
Produce angled louvers, lances and other directional forms under CNC control. The tool rotates through 360 degrees, avoiding separate tools for every orientation.
Less duplicate tooling and lower risk of loading the wrong tool.
Rotary operations remain part of the CNC program.
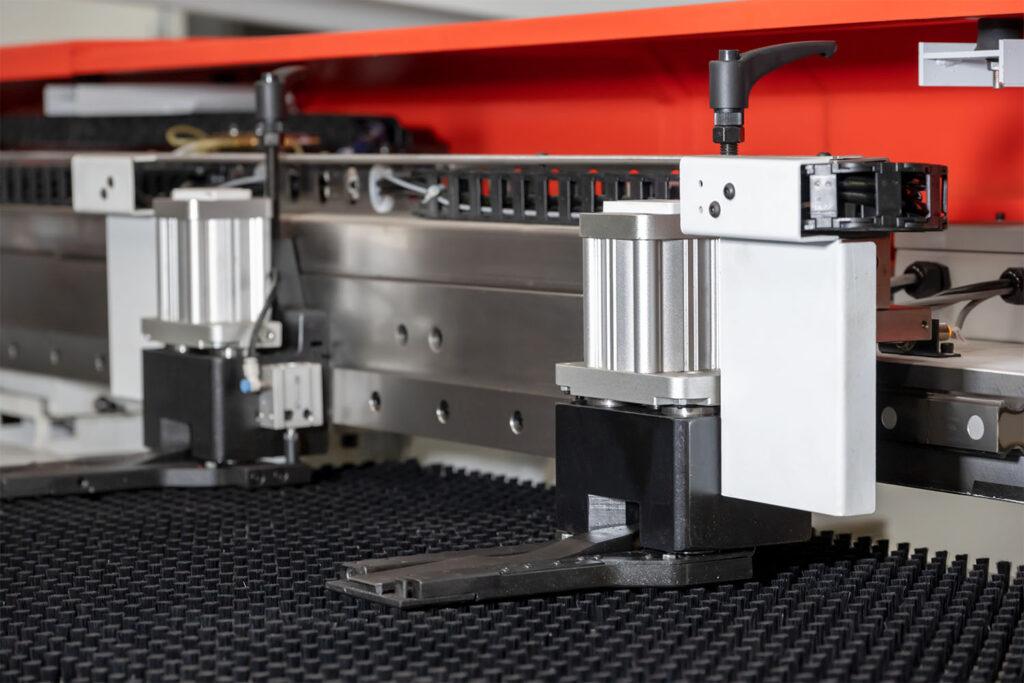
Floating clamp system
Keep the sheet controlled while allowing the required movement during processing. Material-drop detection and clamp protection stop the machine before a misaligned sheet or unsafe stroke causes damage.
Detects sheet movement before the next punch stroke.
Position monitoring helps prevent die-to-clamp collisions.
Protects long nested runs with less operator supervision.
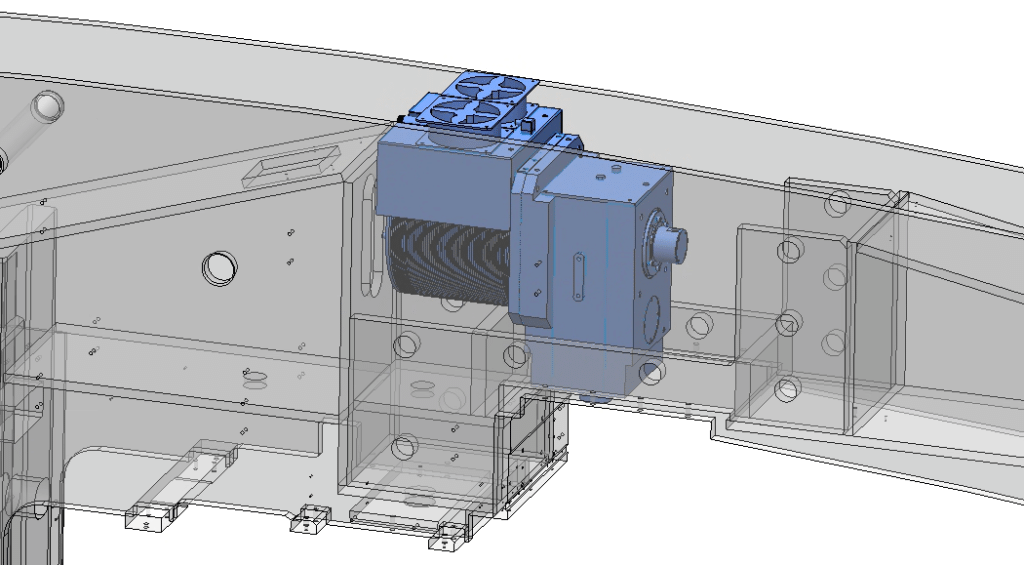
Servo punching drive
The direct-drive servo delivers punching power immediately and uses energy in proportion to the work performed. Air cooling and closed-loop control support stable, repeatable forming.
High-torque direct-drive motor with overload capacity.
Air cooling avoids coolant-related service concerns.
Closed-loop control keeps the forming depth consistent.
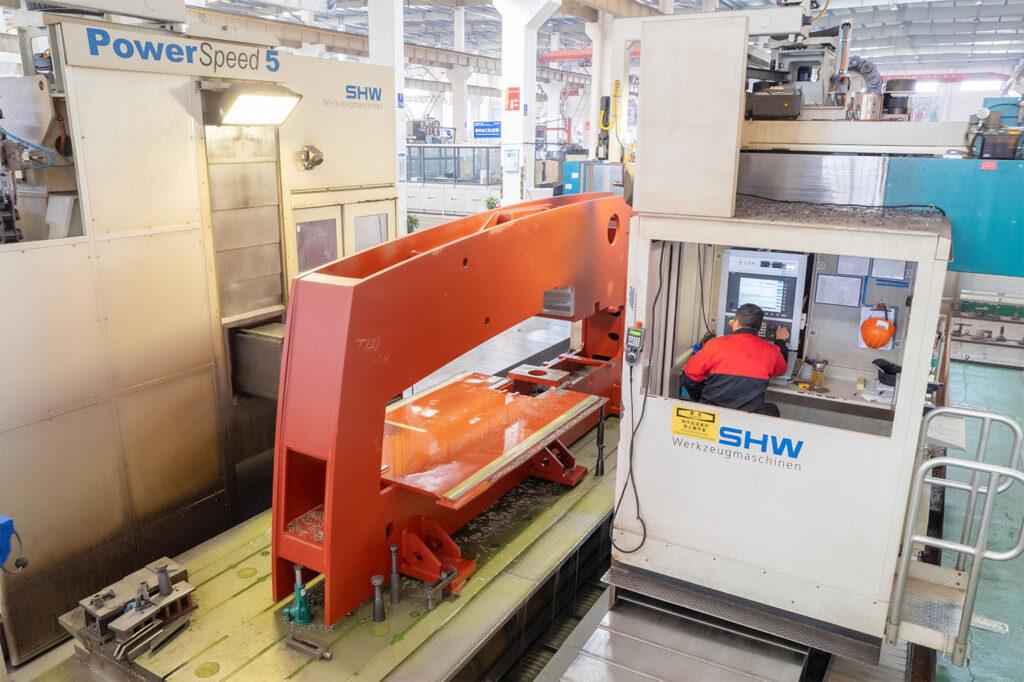
Machine frame
The closed welded frame, five-face SHW machining and finite-element design help keep the machine geometry stable during high-frequency punching. A common coordinate system supports consistent accuracy across the shift.
Rigid closed structure designed to resist deformation.
Key reference surfaces are machined in one coordinate system.
Supports the specified ±0.1 mm punching accuracy.
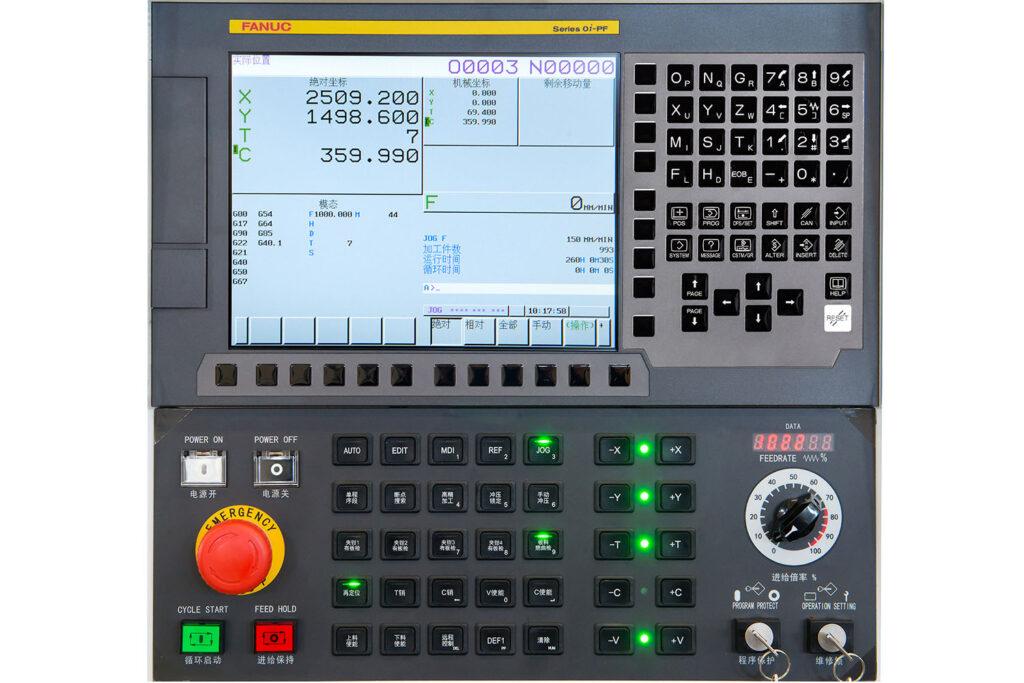
FANUC CNC system
A familiar CNC platform simplifies operation, maintenance and support. Existing FANUC experience can transfer to the MT300E without learning a proprietary control environment from scratch.
Five controlled axes: X, Y, V, T and C.
Familiar diagnostics and service practices.
FANUC support infrastructure is available across major markets.
Date tehnice
| Specification | MT+ 300E-2515 |
|---|---|
| Max. punch force | 300 kN |
| Tip de antrenare principal | Servo motor |
| Dimensiune maximă de procesare a tablei (cu o singură repoziționare) | 5000x1500 mm |
| Grosime max. tablă de prelucrare | 6 mm |
| Max. punch diameter per time | Φ88.9 mm |
| Cursă max. de poansonare | 32 mm |
| No. of clamps | 3 buc |
| No. of stations | 32 pcs |
| Numărul de indexuri automate | 2 (C) pcs |
| Precizie poansonare | ±0.1 mm |
| Max. feeding speed - X Axis | 80 m/min |
| Max. feeding speed - Y Axis | 80 m/min |
| Max. feeding speed - XY Combined | 113 m/min |
| Worktable Selection - For thickness 3 mm and below | Fine brush fixed worktable |
| Worktable Selection - For thickness 3-4 mm | Brush and steel ball fixed worktable |
| Worktable Selection - For thickness 4-6 mm | All steel ball fixed worktable |
| Max. punch hit at 1 mm pitch with 6 mm stroke | 750 hpm |
| Max. punch hit at 25 mm pitch with 6 mm stroke | 400 cp |
| Viteza turelei | 30 rpm |
| Sistem CNC | FANUC |
| No. of controlling axis | 5 (X, Y, V, T, C) pcs |
| Dimension (Including safety fence) | 7026×7900×2360 mm |