Punching is back
Vyrábějte více. Méně nastavujte.
Současně lze osadit 38 nástrojů, takže celé série zakázkové výroby skříní probíhají bez přerušení. Žádná ruční výměna nástrojů během výroby. Méně přestaveb. Více dílů za směnu.
±0,1 mm. Směnu za směnou
Zpracovatelský rám SHW a servopohon s uzavřenou regulační smyčkou zajišťují přesnost děrování ±0,1 mm při nepřetržitém vysokofrekvenčním děrování bez dlouhodobého posunu. Přesnost, kterou můžete garantovat svým zákazníkům.
Méně odpadu. Kratší cykly.
Integrované rozmísťování, kalkulace nákladů a sekvencování zajišťují o 8–15 % lepší využití materiálu než ruční rozvržení. Žádné zkušební řezy, žádný zbytečně spotřebovaný plech. Automaticky kratší cyklové časy.
Programování na autopilota
JFY PUNCH automaticky programuje děrování dílů s optimalizací pořadí, seskupenými nástroji, mikrospoji a bez ručního zadávání. Připojte JFY PLUS a programujte řezání, děrování a ohýbání v jednom rozhraní a jednom pracovním postupu.
Tvary, které laser nedokáže vyrobit
Žaluzie, výtažky, závitové otvory, žebra a průstřihy – vše v jednom programu a na jednom stroji. Pokud vaše díly vyžadují tváření, dokáže ho pouze děrování.
Funkce a výkon
Podrobnosti na
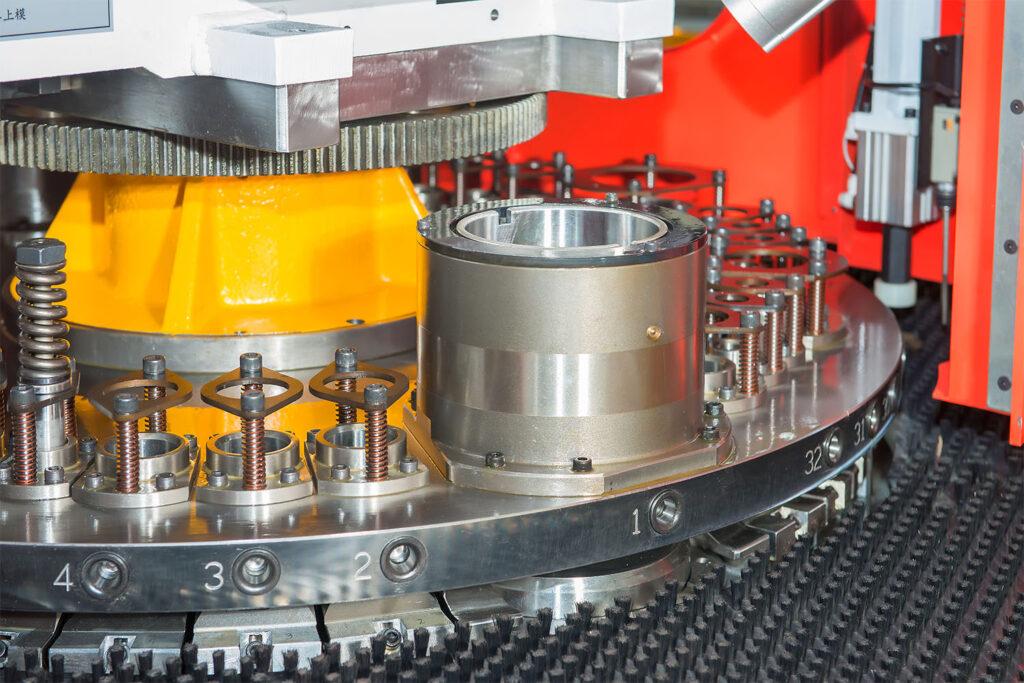
38-station turret
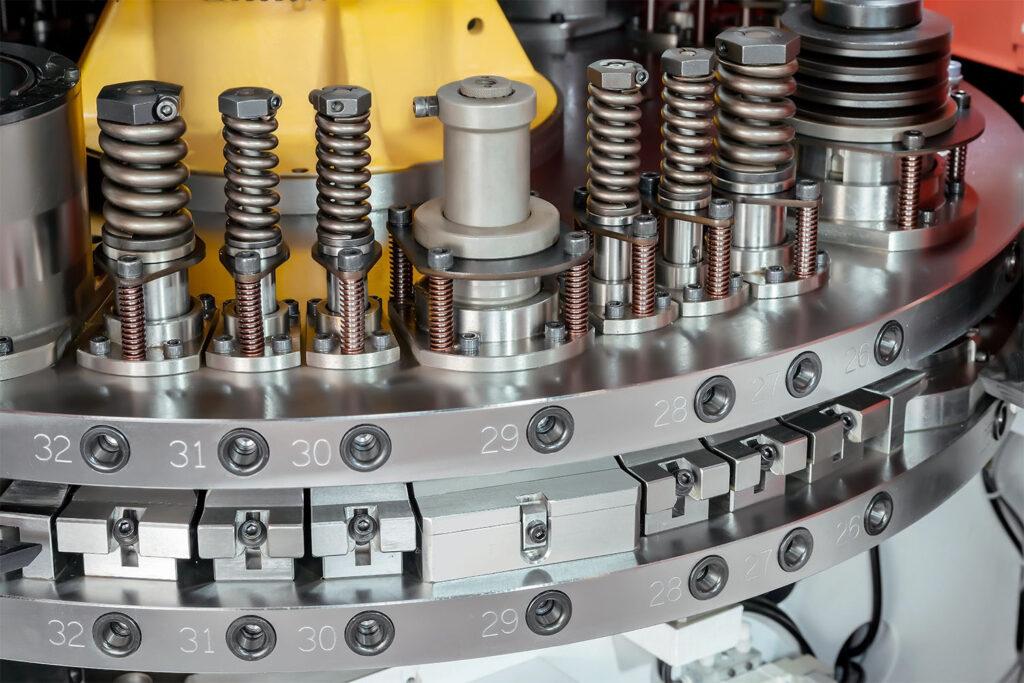
Keep punching, forming, louver and tools loaded at the same time. Fewer tool changes keep batch jobs running instead of waiting for setup.
38 stations for a broad mix of punching and forming tools.
Quick-release lower dies simplify between-job changes.
Supports longer runs with fewer manual interruptions
Auto-index rotary station
Produce angled louvers, lances and other directional forms under CNC control. The tool rotates through 360 degrees, avoiding separate tools for every orientation.
Less duplicate tooling and lower risk of loading the wrong tool.
Rotary operations remain part of the CNC program.
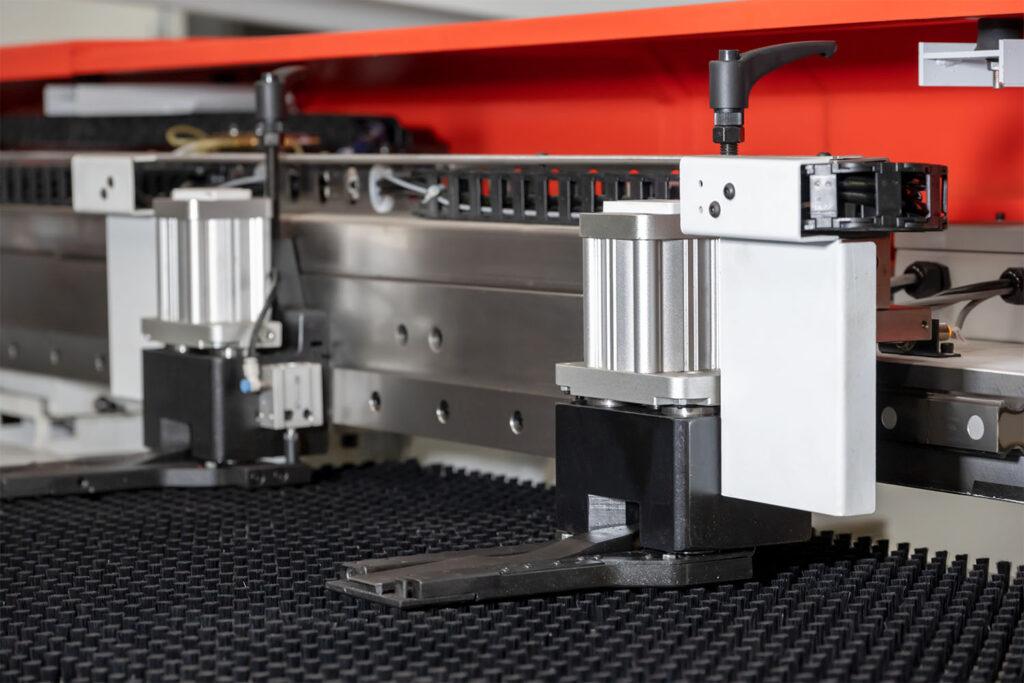
Floating clamp system
Keep the sheet controlled while allowing the required movement during processing. Material-drop detection and clamp protection stop the machine before a misaligned sheet or unsafe stroke causes damage.
Detects sheet movement before the next punch stroke.
Position monitoring helps prevent die-to-clamp collisions.
Protects long nested runs with less operator supervision.
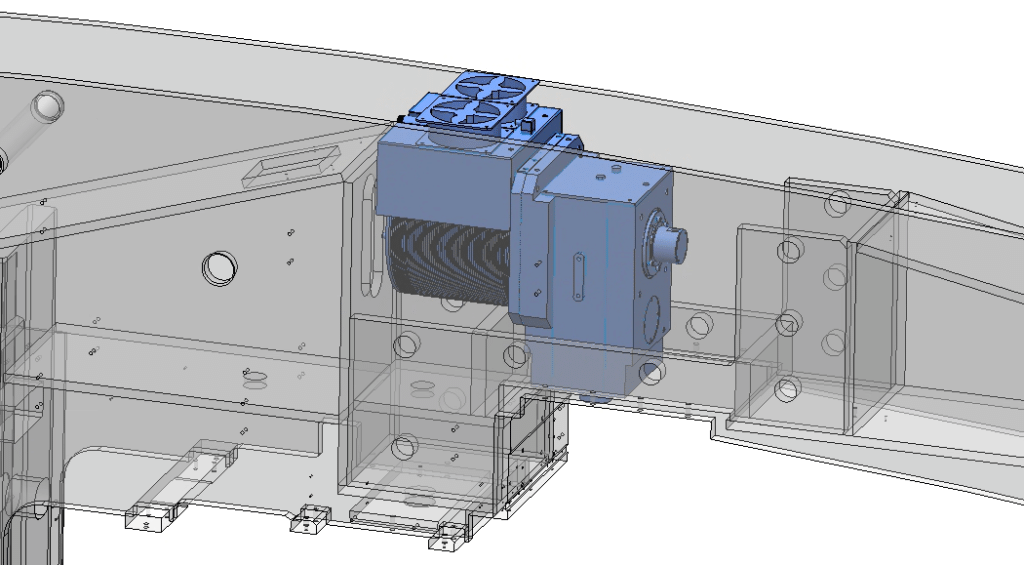
Servo punching drive
The direct-drive servo delivers punching power immediately and uses energy in proportion to the work performed. Air cooling and closed-loop control support stable, repeatable forming.
High-torque direct-drive motor with overload capacity.
Air cooling avoids coolant-related service concerns.
Closed-loop control keeps the forming depth consistent.
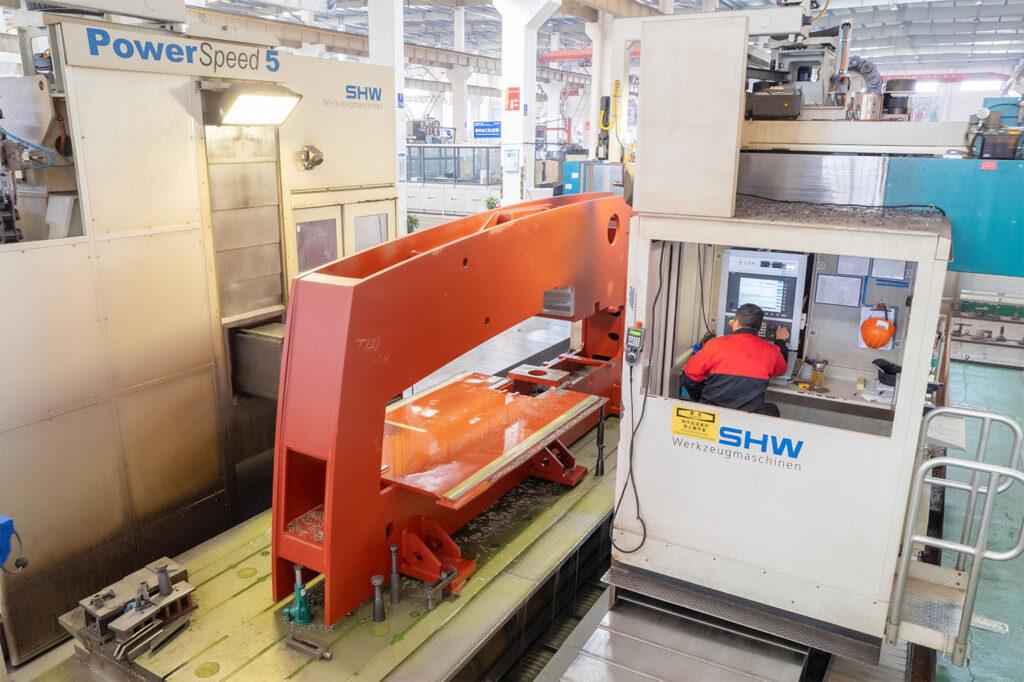
Machine frame
The closed welded frame, five-face SHW machining and finite-element design help keep the machine geometry stable during high-frequency punching. A common coordinate system supports consistent accuracy across the shift.
Rigid closed structure designed to resist deformation.
Key reference surfaces are machined in one coordinate system.
Supports the specified ±0.1 mm punching accuracy.
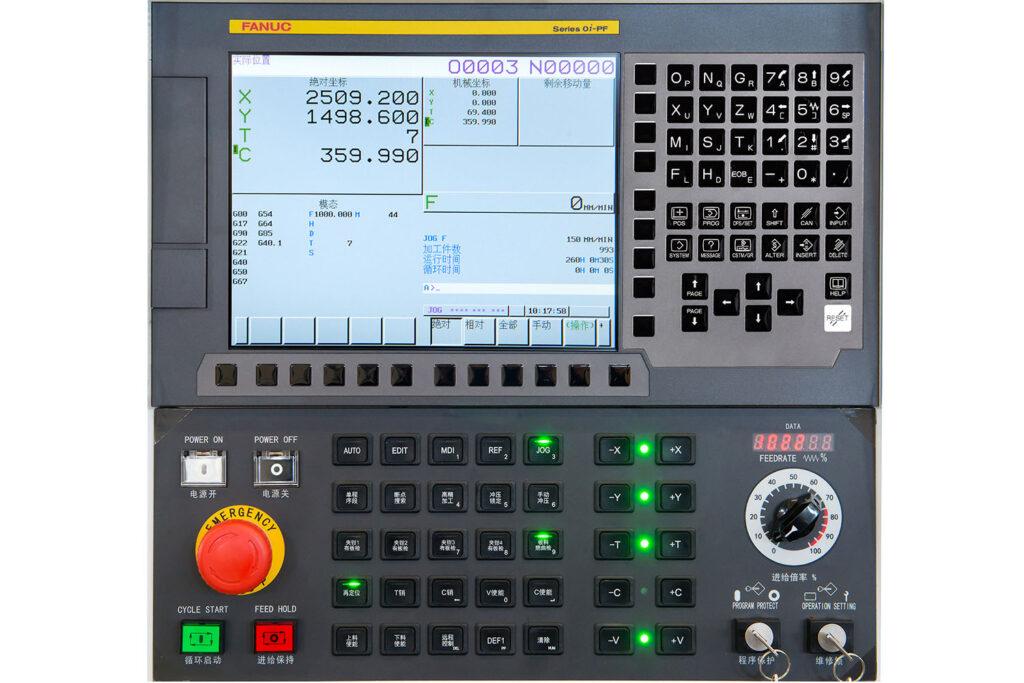
FANUC CNC system
A familiar CNC platform simplifies operation, maintenance and support. Existing FANUC experience can transfer to the MT300E without learning a proprietary control environment from scratch.
Five controlled axes: X, Y, V, T and C.
Familiar diagnostics and service practices.
FANUC support infrastructure is available across major markets.
Technická data
| Specification | MT+ 300E-2515 |
|---|---|
| Max. punch force | 300 kN |
| Hlavní typ pohonu | Servo motor |
| Max. velikost zpracovávaného plechu [s jednorázovým přemístěním] | 5000x1500 mm |
| Max. tloušťka materiálu | 6 mm |
| Max. punch diameter per time | Φ88.9 mm |
| Max. délka zdvihu střihu | 32 mm |
| No. of clamps | 3 ks |
| No. of stations | 32 pcs |
| Počet automatických indexací | 2 (C) pcs |
| Přesnost střihu | ±0.1 mm |
| Max. feeding speed - X Axis | 80 m/min |
| Max. feeding speed - Y Axis | 80 m/min |
| Max. feeding speed - XY Combined | 113 m/min |
| Worktable Selection - For thickness 3 mm and below | Fine brush fixed worktable |
| Worktable Selection - For thickness 3-4 mm | Brush and steel ball fixed worktable |
| Worktable Selection - For thickness 4-6 mm | All steel ball fixed worktable |
| Max. punch hit at 1 mm pitch with 6 mm stroke | 750 hpm |
| Max. punch hit at 25 mm pitch with 6 mm stroke | 400 hpm |
| Rychlost otáčení turetu | 30 otáček za minutu |
| CNC systém | FANUC |
| No. of controlling axis | 5 (X, Y, V, T, C) pcs |
| Dimension (Including safety fence) | 7026×7900×2360 mm |