



Punch efficiency with JFY
Produce more. Set up less.
38 tools load simultaneously, so entire cabinet job families run without interruption. No manual tool swapping mid-run. Less changeover. More parts per shift.
±0.1 mm. Shift after shift
SHW processing frame and closed-loop servo ensures ±0.1 mm hit accuracy under continuous high-frequency punching, with no drift over time. Precision you can quote to your customers.
Less scrap. Shorter cycles.
Integrated nesting, costing, and sequencing deliver 8-15% better material utilization versus manual layout. No trial cuts, no wasted sheet. Shorter cycle times, automatically.
Programming on autopilot
JFY PUNCH programs punching parts automatically with sequence optimization, cluster tooling, micro joints, zero manual input. Connect to JFY PLUS and program Cut, Punch, and Bend in one interface and one workflow.
Forms no laser can make
Louvers, extrusions, tapped holes, ribs, knockouts: all in one program, on one machine. If your parts need forming, only punching delivers it.
Features and Performance
Details
Reliable and Robust Punching Solution
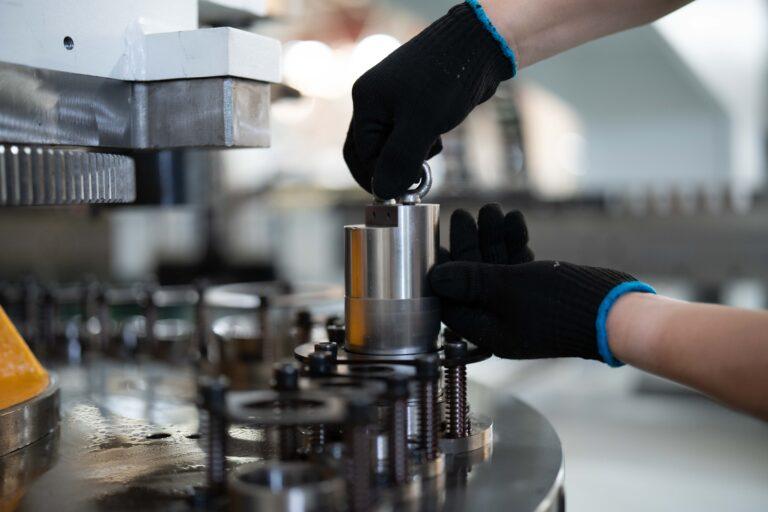
- Direct drive torque servo motor with high overload capacity ensures low energy consumption, high transmission efficiency, and reliable performance.
- Adjustable punch force adapts to sheet thickness and speed for maximum punching quality.
- Advanced floating clamp technology for smooth feeding and automatic clamp protection to prevent tool and clamp damage.
- Standard turret with 32 stations offers ample capacity for a wide range of punching needs, including holes and shapes.
- Convenient maintenance and consistent performance for long-term operation.
Efficient and User-Friendly Programming
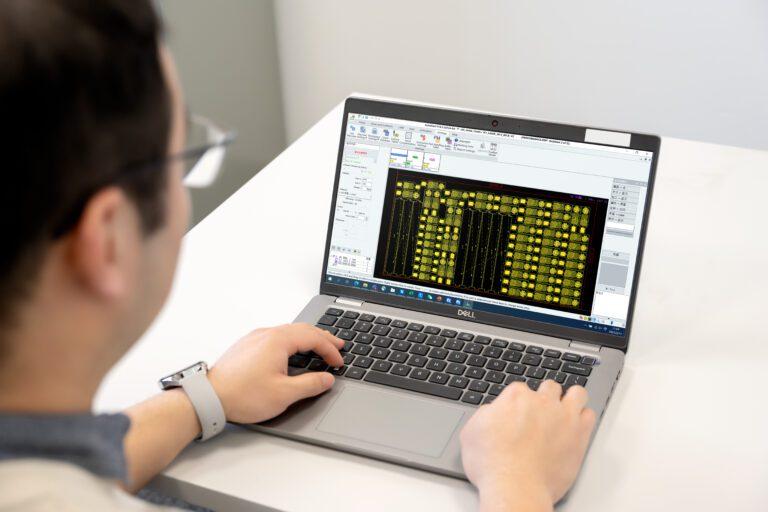
- CNCKAD software converts CAD files into optimized NC code, automating tool selection and minimizing machine runtime.
- Simplified G-code programming for quick and easy operation, supported by the FANUC 0i-PF CNC system for easy and fast operation.
- Features include automatic punching, adaptable microjoints, predefined shapes, and efficient sheet trimming for maximum material utilization.
- Advanced functionality such as customizable turret setup, sheet repositioning, auto indexing, and clamp avoidance for seamless processing.
Technical Data
| Specification | MT300E | ||
|---|---|---|---|
| Max. punch force | 300 kN | ||
| Main driving type | Single servo motor | ||
| CNC system | FANUC CNC system | ||
| Max. sheet processing size (with one time repositioning) | 5000x1250mm | 5000x1500mm | 5000x2000mm |
| Number of clamps | 3 pcs | ||
| Max. processing sheet thickness | 6mm (Mild steel) | ||
| Max. punch diameter per time | Φ88.9 mm | ||
| Max. punch hit at 1mm pitch | 780 hpm | ||
| Max. punch hit at 25.4mm pitch | 400 hpm | ||
| Max. marking speed | 2000 hpm | ||
| Max. punch stroke | 32 mm | ||
| Number of stations | 32 pcs | ||
| Number of auto index | 2 pcs | ||
| Number of controlling axis | 5 (X, Y, V, T, C) | ||
| Tooling type | Long Type | ||
| Max. feeding speed | X Axis | 80 m/min | |
| Y Axis | 80 m/min | ||
| XY Combined | 113m/min | ||
| Worktable Selection | For thickness 3mm and below | Fine Brush Fixed Worktable | |
| For thickness 3-4mm | Brushed Steel Ball Fixed Worktable | ||
| For thickness 4-6mm | All Steel Ball Fixed Worktable | ||
| Turret speed | 30 rpm | ||
| Punching accuracy | ±0.1 mm | ||
| Power supply | 45 kVA | ||
| Air pressure | 0.55 MPa | ||
| Air consumption | 250 L/min | ||
| Dimension | 5260x5200x2360 mm | 5760x5200x2360 mm | 6760x5200x2360 mm |
| Weight | 17000 kg | 18000 kg | 25300 kg |