Punching is back
Produkuj więcej. Ogranicz przezbrojenia.
Jednocześnie można załadować 38 narzędzi, dzięki czemu całe rodziny zleceń na szafy mogą być realizowane bez przerw. Bez ręcznej wymiany narzędzi w trakcie pracy. Mniej przezbrojeń. Więcej części na zmianę.
±0,1 mm. Zmiana po zmianie
Rama obróbcza SHW i serwonapęd z zamkniętą pętlą sprzężenia zwrotnego zapewniają dokładność wykrawania ±0,1 mm podczas ciągłego wykrawania z wysoką częstotliwością, bez dryfu w czasie. Precyzja, którą można zagwarantować klientom.
Mniej braków. Krótsze czasy cyklu.
Zintegrowane nestowanie, kalkulacja kosztów i sekwencjonowanie zapewniają o 8–15% lepsze wykorzystanie materiału w porównaniu z układem ręcznym. Bez próbnych cięć i marnowania blachy. Automatycznie krótsze czasy cyklu.
Programowanie na autopilocie
JFY PUNCH automatycznie programuje wykrawanie części, optymalizując kolejność operacji, grupując narzędzia, stosując mikromostki i eliminując ręczne wprowadzanie danych. Połącz JFY PLUS i programuj cięcie, wykrawanie oraz gięcie w jednym interfejsie i jednym przepływie pracy.
Kształty, których nie można wykonać laserem
Żaluzje, przetłoczenia, otwory gwintowane, żebra i wybijane otwory – wszystko w jednym programie i na jednej maszynie. Jeśli części wymagają formowania, tylko wykrawanie może je wykonać.
Funkcje i wydajność
Szczegóły
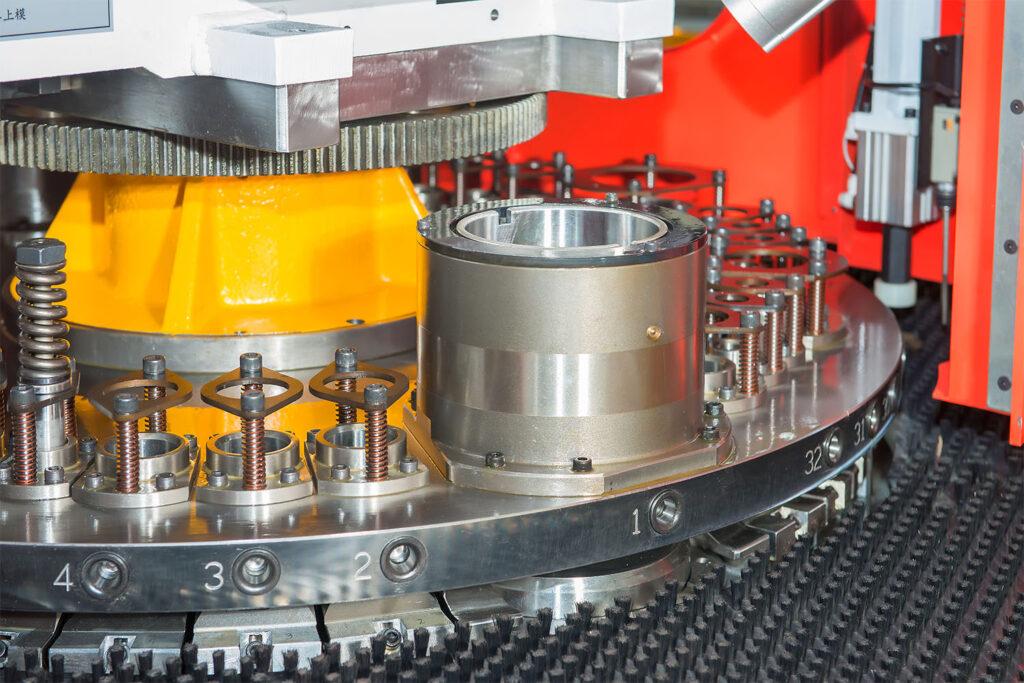
38-station turret
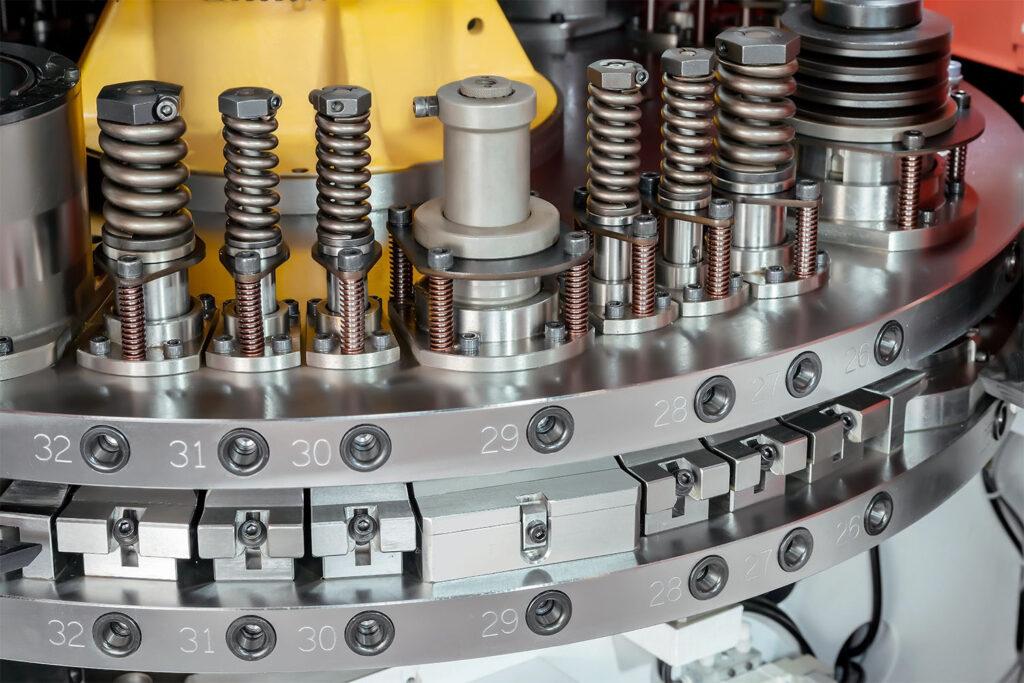
Keep punching, forming, louver and tools loaded at the same time. Fewer tool changes keep batch jobs running instead of waiting for setup.
38 stations for a broad mix of punching and forming tools.
Quick-release lower dies simplify between-job changes.
Supports longer runs with fewer manual interruptions
Auto-index rotary station
Produce angled louvers, lances and other directional forms under CNC control. The tool rotates through 360 degrees, avoiding separate tools for every orientation.
Less duplicate tooling and lower risk of loading the wrong tool.
Rotary operations remain part of the CNC program.
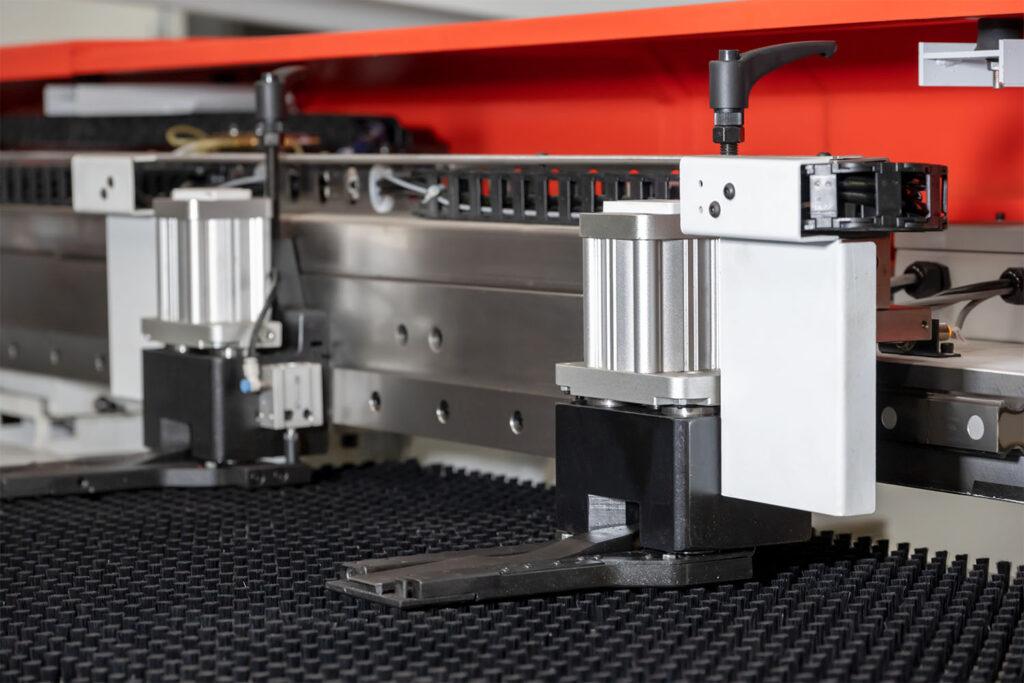
Floating clamp system
Keep the sheet controlled while allowing the required movement during processing. Material-drop detection and clamp protection stop the machine before a misaligned sheet or unsafe stroke causes damage.
Detects sheet movement before the next punch stroke.
Position monitoring helps prevent die-to-clamp collisions.
Protects long nested runs with less operator supervision.
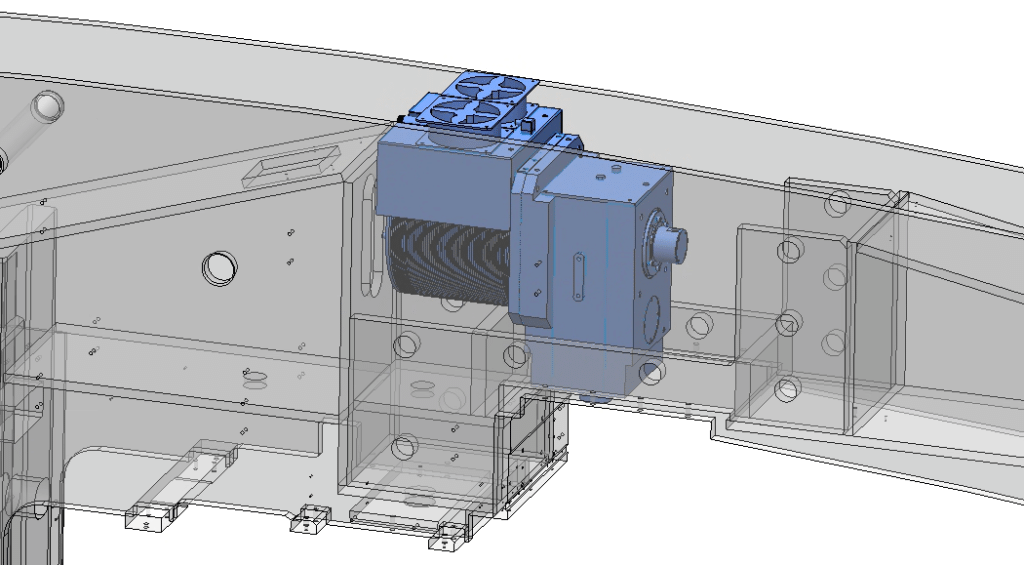
Servo punching drive
The direct-drive servo delivers punching power immediately and uses energy in proportion to the work performed. Air cooling and closed-loop control support stable, repeatable forming.
High-torque direct-drive motor with overload capacity.
Air cooling avoids coolant-related service concerns.
Closed-loop control keeps the forming depth consistent.
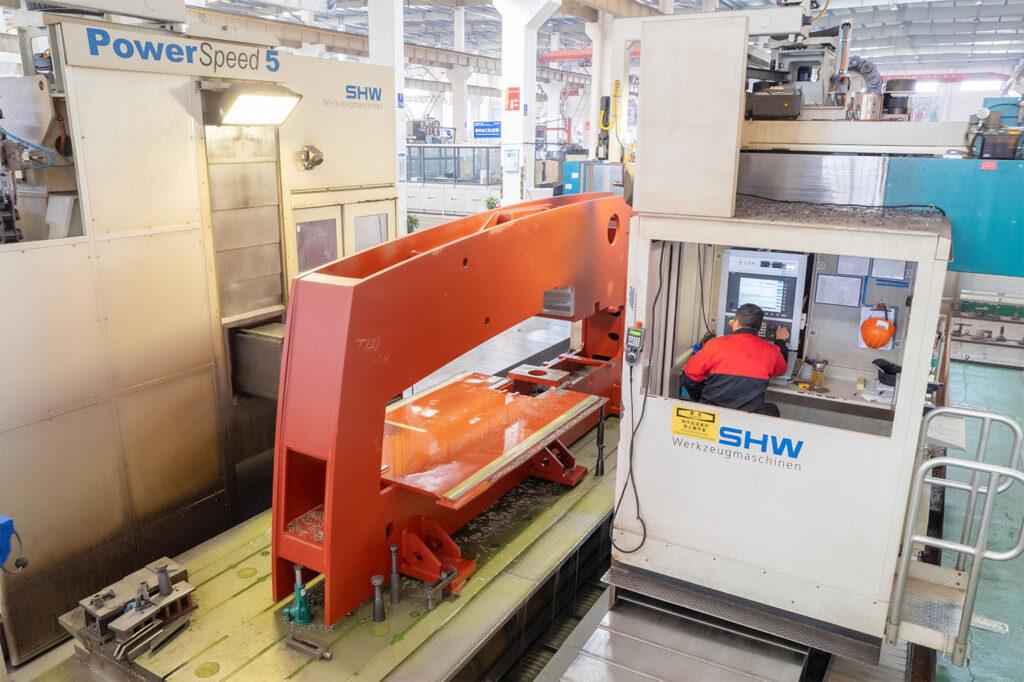
Machine frame
The closed welded frame, five-face SHW machining and finite-element design help keep the machine geometry stable during high-frequency punching. A common coordinate system supports consistent accuracy across the shift.
Rigid closed structure designed to resist deformation.
Key reference surfaces are machined in one coordinate system.
Supports the specified ±0.1 mm punching accuracy.
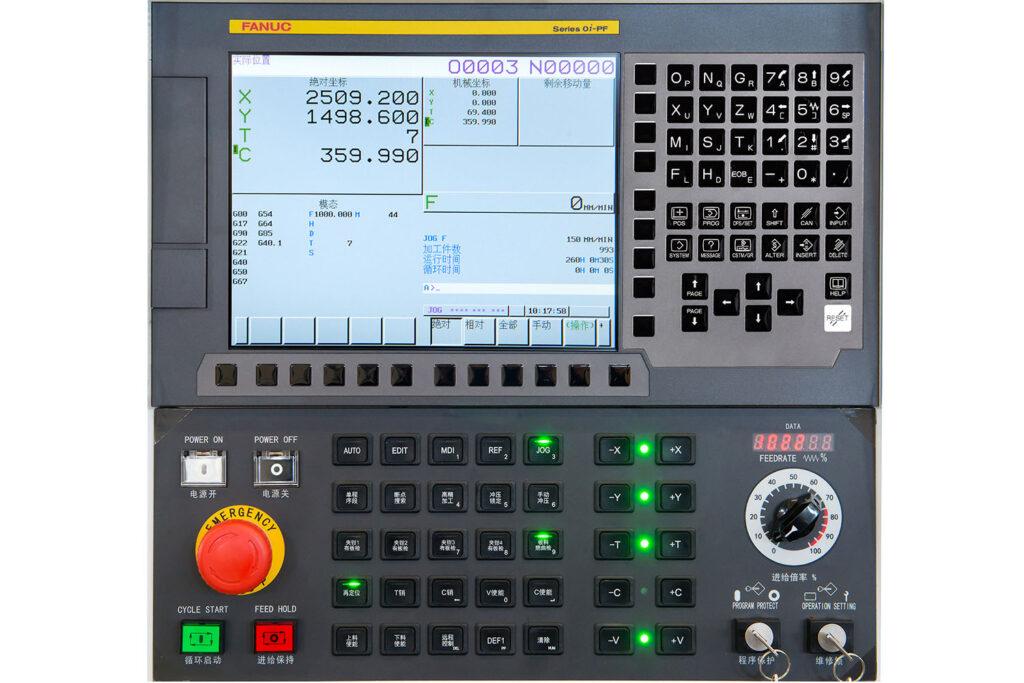
FANUC CNC system
A familiar CNC platform simplifies operation, maintenance and support. Existing FANUC experience can transfer to the MT300E without learning a proprietary control environment from scratch.
Five controlled axes: X, Y, V, T and C.
Familiar diagnostics and service practices.
FANUC support infrastructure is available across major markets.
Dane techniczne
| Specification | MT+ 300E-2515 |
|---|---|
| Max. punch force | 300 kN |
| Typ napędu głównego | Servo motor |
| Maks. rozmiar przetwarzania arkusza (z jednokrotnym repozycjonowaniem) | 5000x1500 mm |
| Maks. grubość blachy obrabianej | 6 mm |
| Max. punch diameter per time | Φ88.9 mm |
| Maks. skok tłoczenia | 32 mm |
| No. of clamps | 3 szt. |
| No. of stations | 32 pcs |
| Liczba indeksów automatycznych | 2 (C) pcs |
| Dokładność tłoczenia | ±0.1 mm |
| Max. feeding speed - X Axis | 80 m/min |
| Max. feeding speed - Y Axis | 80 m/min |
| Max. feeding speed - XY Combined | 113 m/min |
| Worktable Selection - For thickness 3 mm and below | Fine brush fixed worktable |
| Worktable Selection - For thickness 3-4 mm | Brush and steel ball fixed worktable |
| Worktable Selection - For thickness 4-6 mm | All steel ball fixed worktable |
| Max. punch hit at 1 mm pitch with 6 mm stroke | 750 hpm |
| Max. punch hit at 25 mm pitch with 6 mm stroke | 400 obr./min |
| Prędkość wieży | 30 obr./min |
| System CNC | FANUC |
| No. of controlling axis | 5 (X, Y, V, T, C) pcs |
| Dimension (Including safety fence) | 7026×7900×2360 mm |